Model BF230-10 Bell Furnace adopts Kanthal heating elements
|


|
Model BF230-10 Bell Furnace adopts Kanthal heating elements The performance of the heating element directly determines the
heating efficiency and service life of the furnace. The Model BF230-10 Bell-Type Furnace is exclusively equipped
with Kanthal heating wires. As a core component made of professional heating alloys, it
guarantees the performance of the furnace with its excellent
material properties. Product Description Model: BF230-10 Bell Furnace Application This equipment is mainly designed for LTCC sintering, it can also be used for binder burning out and sintering process of other relevant electrical products. Technical Specification
Composition of Furnace Structure The equipment is mainly composed of outer frame, chamber, bottom support, lifting system and control system. 1. Chamber Design The chamber is made of ceramic fiberboard and fiber products, and the outermost layer is surrounded by calcium silicate board. The inner layer is surrounded by ceramic fiber heating plate, from top to bottom 4 groups of heating, independent temperature control. The booster air intake box is provided on the right side, and the exhaust gas collection and exhaust box are provided on the left side. The chimney outlet is installed with an auxiliary exhaust amplifier to ensure that the exhaust gas generated during the sintering process can be discharged in time. 2. Bottom Support Design The equipment is equipped with lifting base support, which can be loaded after lowering. For safety reasons, the equipment heating and lifting control are interlocked. The bottom plate is mechanically locked in the working position during heating process. The heating process would not start until the bottom plate is locked. There is a sealing layer between the bottom plate and the chamber to prevent the heat loss from gap through the intersection at high temperature. 3. Lifting System The lifting drive system is located at the bottom of the equipment. The lifting platform is lead screw driving. The whole moving process is that the deceleration motor drives the main wheel and the synchronous belt at the same time drives the four synchronous belt wheels connected to the bottom of the wire bar. The lifting system is stable and reliable. when the bottom plate falls down, open the two front doors, push the shift out button, the bottom plate would move out to load and unload. The lifting control with 3 ways, up, down and stop to make the bottom support start and stop at any height. 4. Control System FEC(Fully Enclosed Coil) heating plates are at all 4 sides of chamber, the height direction of 4 groups of heating, 4 points of independent temperature control. The temperature control uses imported temperature control module for each temperature zone, and the data sampling enters the centralized management and control of the touch screen operating system. To adjust the temperature, the output ratio of each temperature zone is uniformly controlled by the touch screen monitor. All 4 heating sections were independently controlled by the N-Type thermal couple, controlling the stability of ±1ºC. Thermal coupling detects the chamber temperature, then send the signal to the temperature control module to control the power module output, so as to obtain accurate temperature control effect. All electrical strong panels connected to the furnace body are installed at the rear of the heating furnace body to provide the most reliable safety protection. In addition, the heating and lifting interlock, the heating function cannot be opened when the bottom plate is opened. 5. Atmosphere System During the use of the equipment, dry, clean and oil-free compressed air can be inputted the furnace through the equipment pipeline system. The air flow is controlled by the glass rotor flowmeter with a single range of 24-240L/min. To avoid the disturbance of low temperature gas in the furnace, the gas is preheated by the heater before entering the furnace. The preheating temperature can be controlled by the temperature controller, and the max preheating temperature is 500ºC. After preheating, the gas is discharged from the pressurized air intake box on the right side of the furnace, and is discharged through the left gas collection and exhaust box. To control the discharge speed of the exhaust gas in the furnace, the exhaust aid system is installed at the chimney outlet which controlled by a flowmeter range 24-240L/min. 6. Real-time touch screen monitoring
Certifications FAQ 1. What products does Chitherm offer? We provide customers with high-quality bell furnaces, hot air furnaces, box furnaces, tube furnaces, vacuum furnaces, car bottom furnaces, rotary kilns, mesh belt furnaces, and pusher furnaces. 2. What pre-sales services does Chitherm provide? We offer timely consultation services to help customers select the most suitable products, along with highly customizable solutions to meet your specific requirements. 3. What are Chitherm's core strengths? As a high-tech enterprise integrating R&D, manufacturing, and sales, Chitherm possesses patented technologies and core resources to deliver superior solutions. |
||||||||||||||||||||||||||||||||||||
| Product Tags: Bell furnace with Kanthal heating Elevator furnace heating elements Model BF230-10 bell furnace |
|
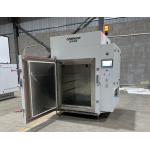
HRF930-05 Hot Air Box Furnace with 900×900×1150mm Chamber, SUS304 Stainless Steel and 4300 m³/h Air Volume |
|
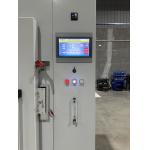
Model HRF930-05 Hot Air Box Furnace with Hot Air Circulating for Electronic Ceramic Powder Curing in 900×900×1150mm Chamber |
|
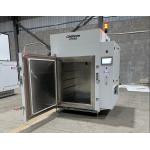
Model HRF930-05 Hot Air Box Furnace with High Uniform Hot Air Circulating and 900×900×1150mm Chamber Dimensions for ±1℃ Temperature Control Stability |
|
HRF930-05 hot air box furnace, precision hot air circulating box furnace, heat treatment aging annealing box furnace |
|
Model RF930-05 Hot Air Box Furnace, High-Temperature Uniform Hot Air Circulating Box Furnace, Non-Standard Customizable |
|
Model HRF930‑05 Hot‑Air Circulating Chamber Furnace, Industrial Furnace for Heat‑Treatment Debinding & Curing |